EN
how disposable nitrile gloves of know if
2026/11/12
Understanding the packaging of nitrile gloves is crucial for B2B buyers, especially when considering bulk purchases. A common inquiry relates to how many nitrile gloves are in a box, which can greatly influence decision-making regarding pricing, storage, and inventory management. We'll explore various box sizes, the relationship between box counts and quality, how to evaluate reliable suppliers, and strategies for using nitrile gloves powder free from bulk boxes effectively. We aim to equip purchasing managers, distributors, engineers, and product managers with the necessary knowledge to make informed decisions in their procurement processes.
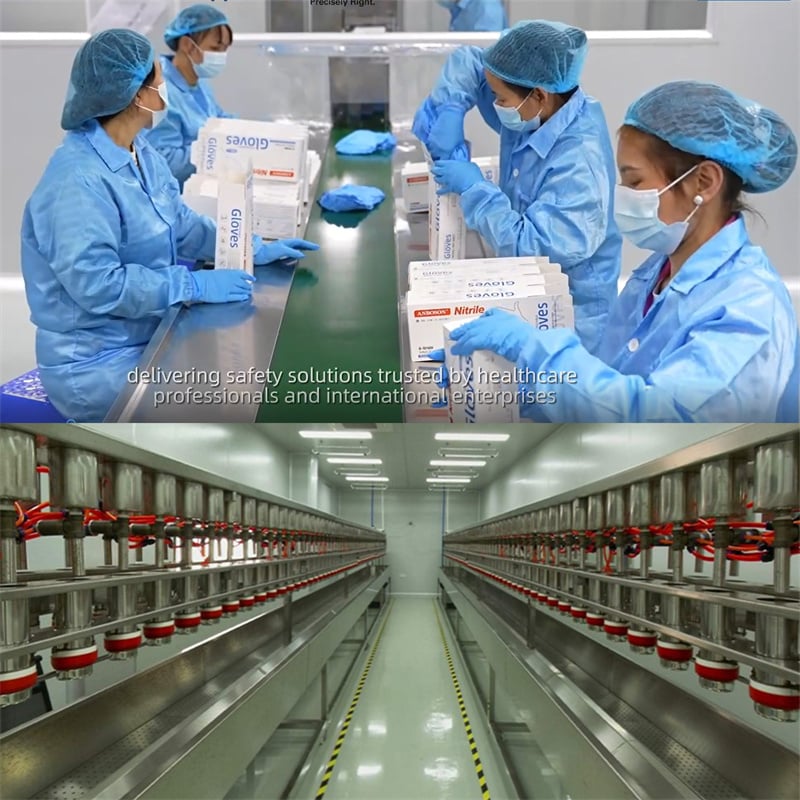
Nitrile gloves are typically packaged in boxes of varying sizes, with the most common counts ranging from 50 to 100 gloves per box. The choice of box size can depend on several factors, including the intended use, storage space, and budget considerations. For example, in healthcare settings, smaller boxes (50 gloves) may be preferred for easy handling and to minimize waste, as they can be used quickly and replaced often. On the other hand, larger boxes (100 gloves) are often favored in industrial settings where gloves are used more frequently, providing better value and reducing the frequency of reordering. Understanding these box sizes helps buyers to manage inventory effectively, ensuring that they have an adequate supply without overstocking. Moreover, different manufacturers may offer unique packaging configurations based on their production capabilities. Anboson Technology, for instance, utilizes advanced chlorination technology to enhance the performance and durability of its nitrile gloves, ensuring that each box delivers consistent quality and value.
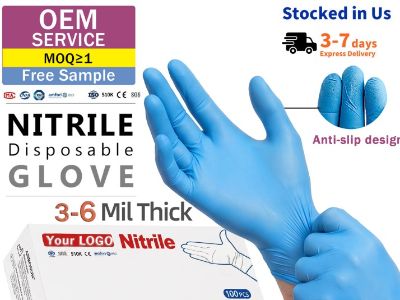
The count of nitrile gloves in a box is not just a matter of quantity; it also relates closely to the quality of the gloves provided. Higher box counts often correlate with lower per-unit costs, which can influence purchasing decisions. However, buyers should consider that quality must not be compromised for quantity. To ensure high-quality free nitrile gloves, buyers should check for certifications such as ISO and CE, which indicate compliance with international safety and quality standards. Anboson Technology's gloves are ISO/CE certified, ensuring that they meet rigorous quality benchmarks. Additionally, buyers should conduct quality inspections upon receiving their orders, looking for signs of defects or inconsistencies in glove thickness, texture, and material integrity. When placing bulk orders, it’s advisable to request samples from suppliers to evaluate the gloves first-hand. This step helps confirm that the product meets the necessary specifications and application requirements before committing to larger quantities.
Choosing a reliable supplier is essential for ensuring consistent quality and timely delivery of nitrile gloves. When assessing potential suppliers, buyers should examine their production capacities and experience. Companies like Anboson Technology, with 20 years of experience, provide a level of assurance regarding their manufacturing capabilities, ensuring that they can meet client demands across various industries. Buyers should also consider the supplier's flexibility in box sizes. Reliable suppliers can accommodate specific requests for box counts based on the client's operational needs. For instance, if a healthcare facility requires smaller boxes for ease of use, a responsive supplier will be able to provide options that align with those requirements. It’s also beneficial to evaluate the supplier’s customer service and support. Clear communication regarding lead times, pricing, and any potential issues is crucial, especially when placing large orders. Building a solid relationship with a trusted supplier can lead to better pricing negotiations and improved service in the long run.
To maximize the efficiency of nitrile gloves sourced from bulk boxes, buyers should develop a systematic approach to inventory management. This includes organizing storage areas to facilitate quick access to gloves and implementing a first-in, first-out (FIFO) system to ensure that older stock is used before newer stock. Additionally, training staff on proper glove usage and disposal can enhance safety and reduce waste. For example, in industrial settings, employees should be encouraged to wear gloves only when necessary and to dispose of them correctly to minimize contamination risks. It's also important to monitor glove usage rates to forecast future orders accurately. By analyzing consumption patterns, companies can adjust their purchasing strategies to ensure they are not over- or under-stocked, thereby optimizing their supply chain and cost management.
While box counts are a practical consideration, they can also raise quality concerns. Buyers should be cautious of unusually low prices associated with bulk box purchases, as these may indicate inferior quality. A lower unit price might not reflect a lower total cost if the gloves do not perform adequately or require more frequent replacement. Furthermore, buyers should verify that the box counts align with their quality expectations. For instance, gloves that are produced in high volumes may undergo less stringent quality control, leading to variability in performance. This is particularly critical in sensitive environments like healthcare where glove integrity is paramount. Engaging with manufacturers to understand their quality control processes can provide insights into the reliability of their products. Companies like Anboson Technology, with robust quality systems in place, demonstrate a commitment to maintaining high standards, ensuring that each box of nitrile gloves blue powder free delivers the performance expected by the buyer. Understanding how many nitrile gloves are in a box and the implications of box size and quality is vital for B2B buyers. By focusing on reliable suppliers, efficient usage, and quality management, purchasing managers and product managers can make informed decisions that not only meet their operational needs but also enhance safety and compliance in their environments.
2026/11/12
2026/11/11
2026/11/10
2026/11/08
2026/11/07
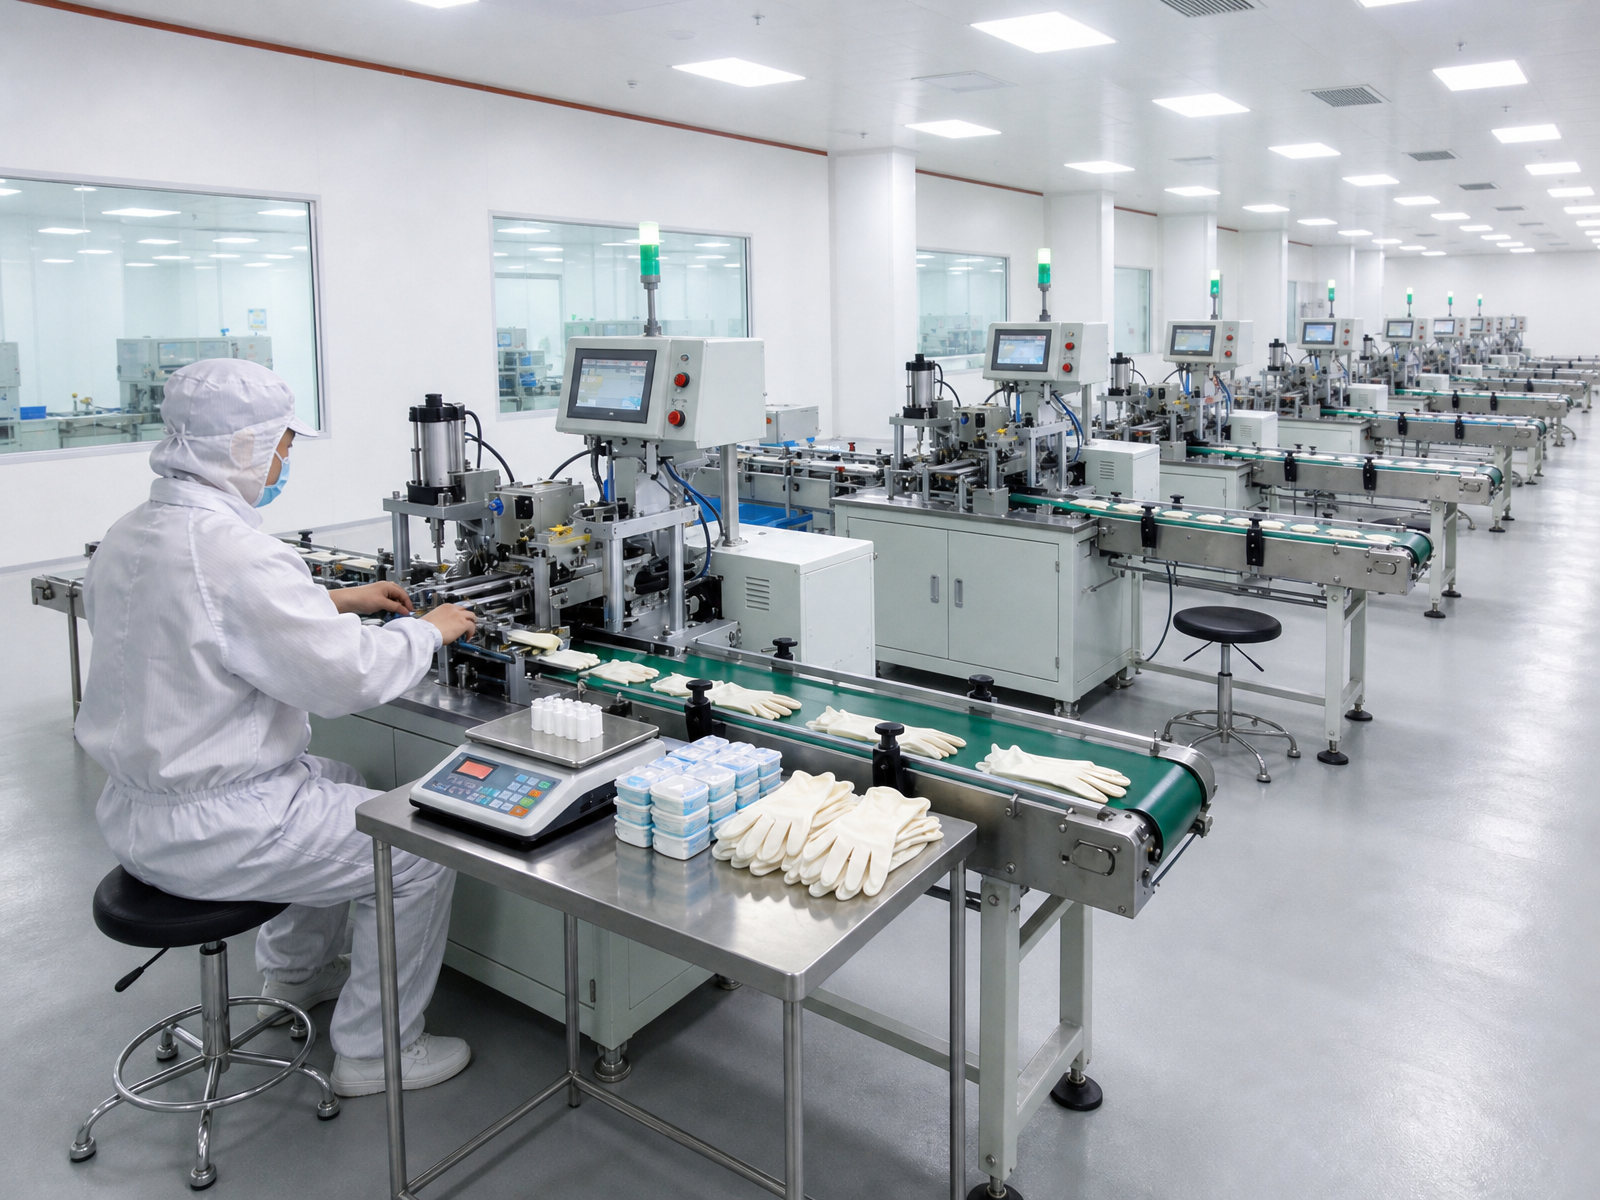
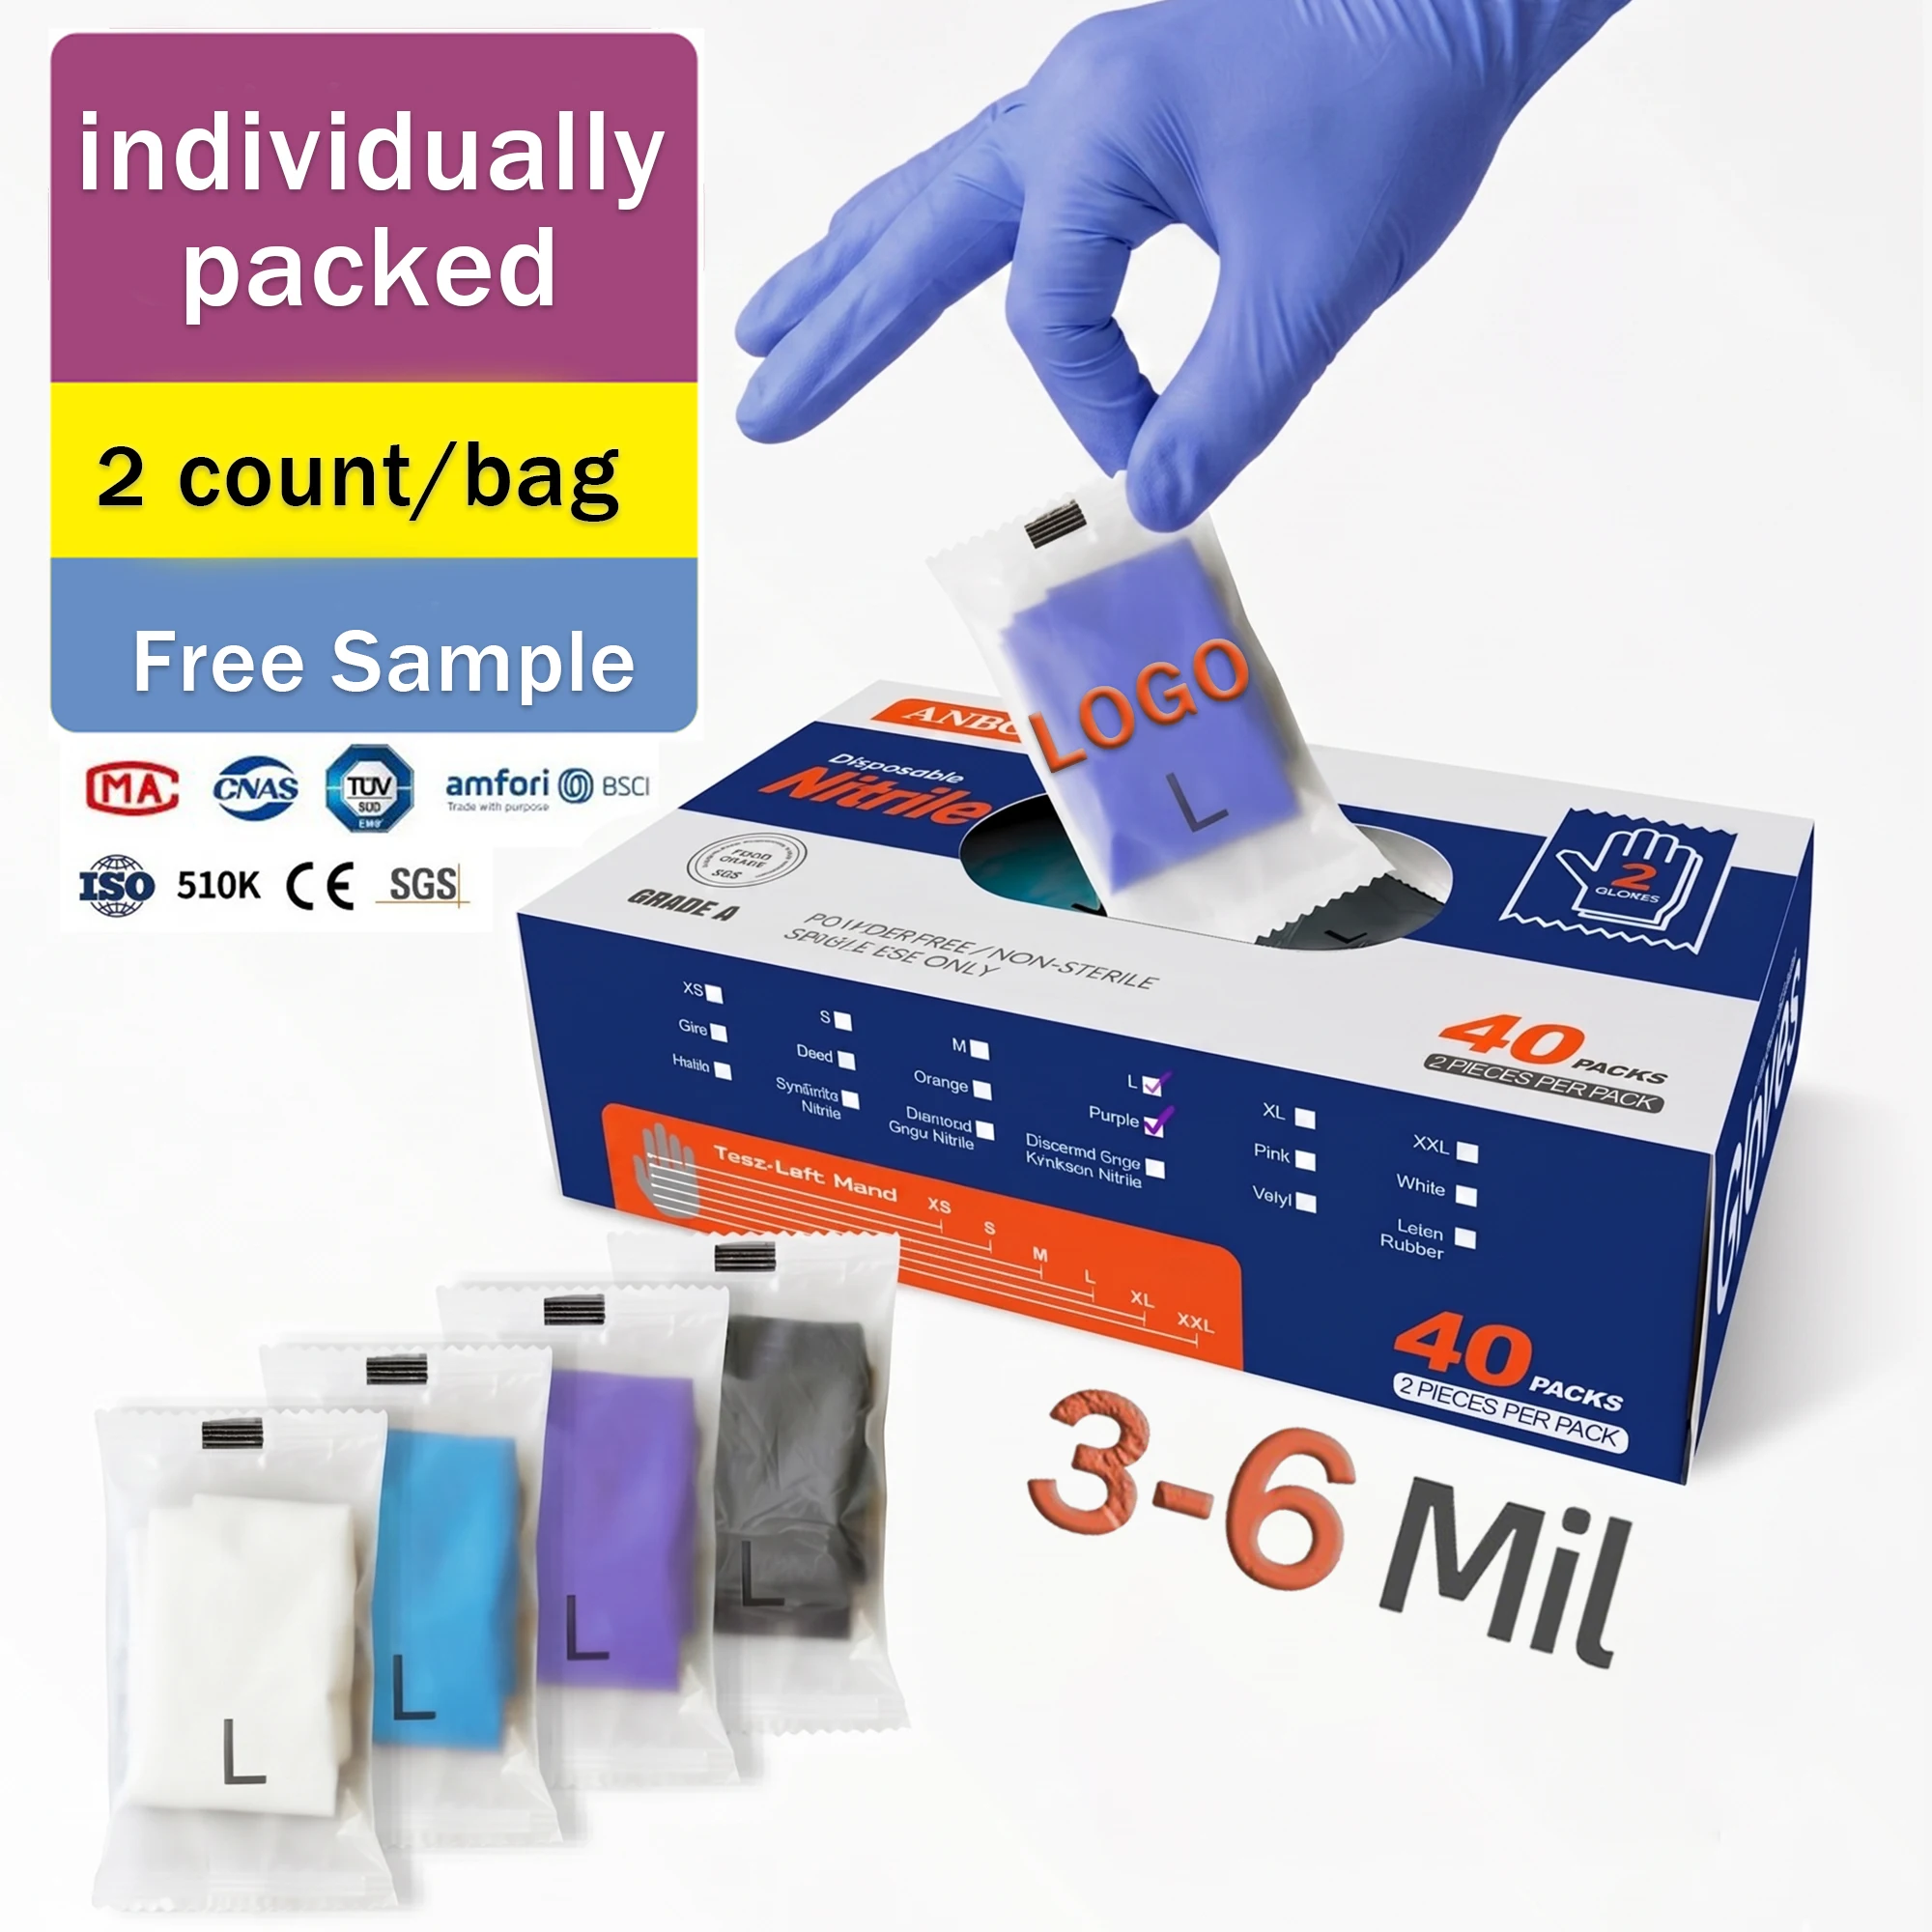
From your logo to your spec, we turn your brand vision into certified reality. Our automated clean-room factory delivers fully customized OEM/ODM nitrile gloves with complete compliance support — FDA 510K, CE, ISO 13485, SGS and more. Low MOQ, free samples, 100% QC on every batch, and responsive after-sales — partner with us for worry-free, certified supply.